China Roller Conveyor Shot Blasting Machine Manufacturer: Key Considerations for Industrial Buyers
2026-08-25
Choosing the right roller conveyor shot blasting machine can make or break your surface preparation workflow. Yet, with so many Chinese manufacturers claiming excellence, how do industrial buyers separate true engineering capability from empty promises? This guide cuts through the noise—starting with what matters most and why PuHua stands out in a crowded field.
The Spec Sheet Won't Tell You How the Machine Handles Your Exact Parts
A machine's brochure will list spindle speeds, axis travel, and table size, but none of that tells you how the tool actually behaves when your part is clamped in place. The way a machine handles your exact geometry—the chatter on a thin wall, the deflection in a deep pocket, the surface finish on a contoured face—only shows up when you push it with your own material and your own cutting strategies. Spec sheets describe a machine in a vacuum; your parts never run in a vacuum.
The real test comes from variables no chart can capture: how the spindle reacts under a sudden load change when you plunge into an interrupted cut, how the way covers and chip evacuation work when your particular chip shape piles up, or whether the coolant nozzles actually reach the cutting zone you care about. These are the details that separate a machine that merely meets its published numbers from one that produces consistent, predictable results on the parts you make every day.
That's why you can't shortcut the process with a data sheet alone. You need to see your part running—the same tool paths, the same fixtures, the same speeds and feeds—before you know whether a machine is truly capable. The only honest answer is a test cut that mirrors your real work. Everything else is just marketing and geometry you already knew before you walked in the door.
Where Manufacturers Cut Corners: Frame Thickness, Turbine Quality, and Dust Collection
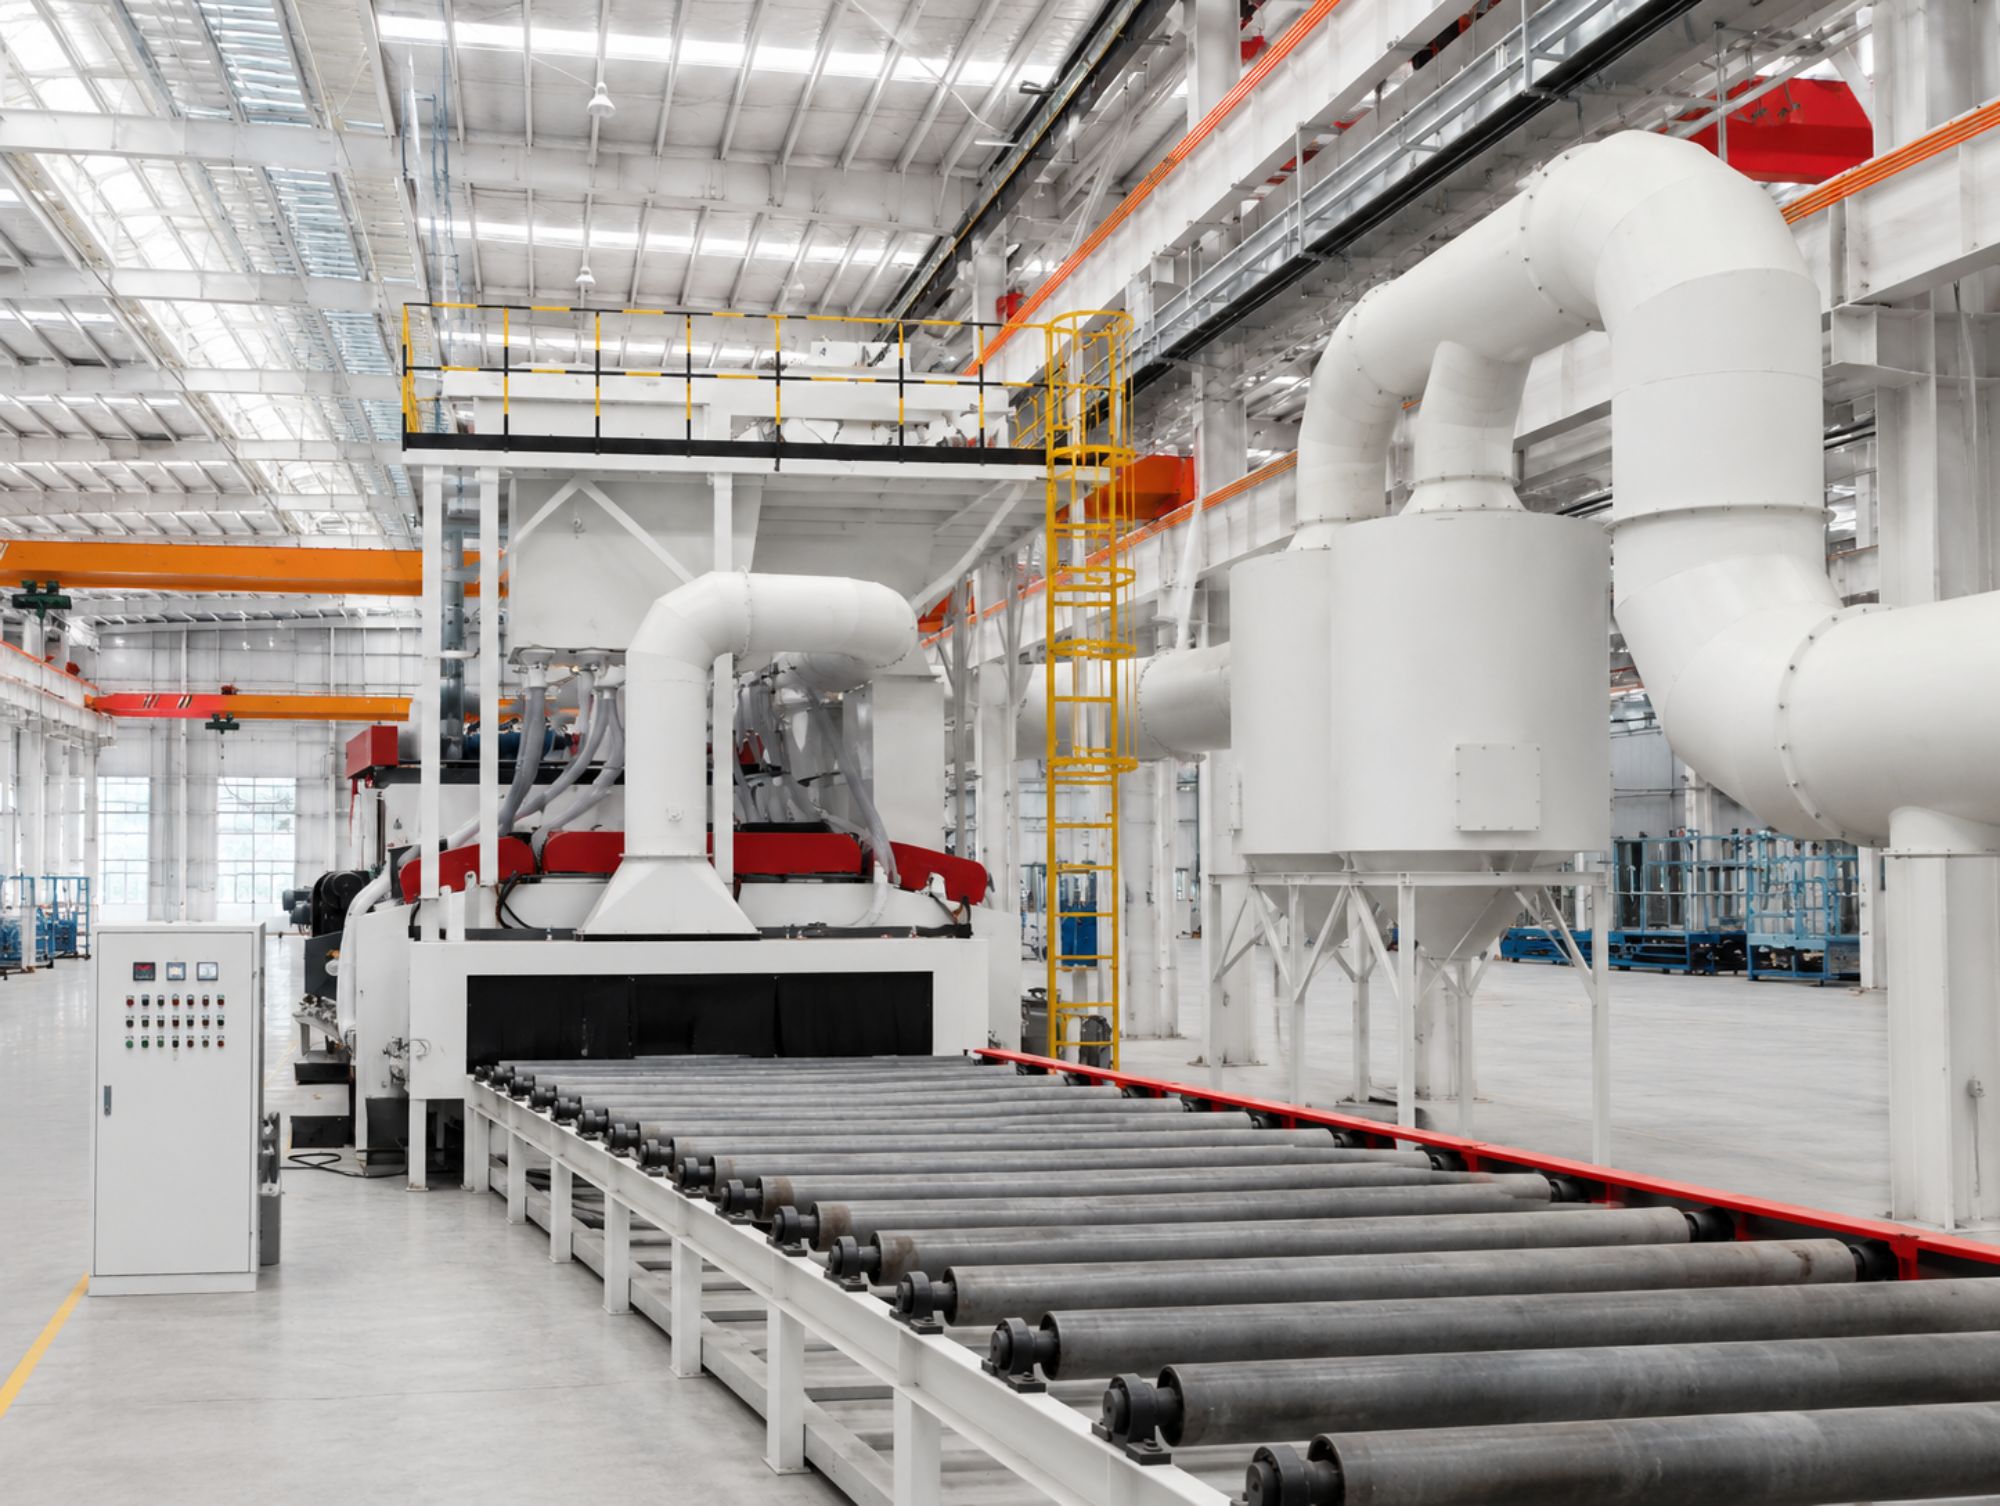
Thin steel frames are easy to spot if you know where to look. Manufacturers trying to hit a price point often shave the gauge down to 1.2 mm or less on machines that see daily use. That flex you feel when pushing a board through isn't just annoying—it translates into uneven cuts and premature bearing wear. A rigid frame should stay flat under load, but many budget models will twist enough to throw a fence out of square after a few months.
The turbine is another place where savings quietly add up. Cheap impellers are often cast rather than machined, leaving rough surfaces that disrupt airflow. Combine that with undersized motors and you get a dust collector that sounds busy but barely moves 600 CFM at the inlet. Ducting and hood design matter too. A narrow port or sharp bend right at the shroud can choke an otherwise decent turbine, leaving fine dust hanging in the air long after the tool stops.
Dust collection often gets treated as an afterthought, with small bags and short filter cartridges that clog fast. When the filter area shrinks, static pressure drops and the whole system loses suction. Some manufacturers also skip a proper cyclone or separator, forcing the impeller to chew through debris. That leads to chipped blades and early motor failure. If a machine ships with a 30-micron bag instead of a 0.5-micron cartridge, you can bet other components were compromised too.
Matching Blast Media and Conveyor Speed to Avoid Rework and Jams
Choosing the wrong blast media for your conveyor speed often turns a routine surface prep job into a parade of clogged nozzles, uneven profiles, and parts circling back for a second pass. Fine grit moving too slowly can pile up in tight corners, while coarse abrasive flying past at high velocity may chew through thin edges before you even notice. The real issue isn’t just the media itself—it’s how the feed rate and conveyor pace either work together or fight each other.
A practical way to sidestep most rework is to match media size to the dwell time under the blast stream. For example, if your conveyor runs at 6 feet per minute with a dense part load, switching from a heavy steel grit to a slightly lighter aluminum oxide blend can prevent media from embedding in soft substrates. Conversely, speeding up the belt while using a finer abrasive often creates a dusty, low-impact cloud that barely etches the surface, forcing operators to slow down and accept a bottleneck. Watch the media recovery system too—when the conveyor outpaces the reclaimer, you’ll see fresh abrasive mixed with spent fines, which leads directly to jams in the metering valve.
Instead of guessing, run a short trial with a tape mark on the belt and a stopwatch. Adjust conveyor speed in small increments while keeping the blast pressure steady, and check the profile depth after each pass. If you notice media bouncing off angles or building up in recesses, either increase the conveyor speed slightly to clear the surface faster or switch to a media with a lower bulk density. That single tweak often eliminates the need for manual touch-ups and keeps the line moving without those frustrating mid-shift stoppages.
Spare Parts and Service After the Sale: What Chinese Suppliers Really Offer
The conversation usually stops once the invoice is paid. That is precisely where the real test of a supplier begins. Many buyers assume that sourcing spare parts from China means long lead times, miscommunication, and an eventual dead end. Yet a growing number of Chinese manufacturers have shifted their focus from simply shipping products to building a full after-sales ecosystem. The difference often comes down to whether the factory treats replacement parts as a burden or as a competitive advantage.
So what can you actually expect? First, clarify the supplier's definition of "available spare parts." Some factories only keep components for current production runs, leaving older models without support. Others maintain dedicated after-sales inventory, complete with part numbers and online catalogs. Ask for a written spare parts policy that covers minimum order quantities, packaging standards, and shipping methods. A factory that can provide a parts list with clear pricing and expected dispatch times is signaling that they intend to stay in business with you beyond the initial order.
Service after the sale also extends to technical support. The best suppliers offer remote troubleshooting via video call, detailed installation guides, and sometimes even on-site training for your local technicians. These are not standard offerings across the board, so you need to ask specific questions: How quickly will they respond to a technical inquiry? Do they have an English-speaking service team? Will they honor warranty claims without requiring you to ship the entire unit back to China? The answers reveal whether a supplier sees you as a one-time customer or a long-term partner.
Verifying Performance Claims Before the Deposit Leaves Your Account
Before any money moves out of your account, ask for evidence that goes beyond glossy brochures and polished sales decks. A legitimate performance claim should be backed by raw test data, a clear description of the measurement conditions, or verifiable client outcomes. If the numbers only appear in a marketing email and cannot be traced to an original source, treat that as a warning sign.
Reach out to current or past customers directly instead of relying solely on curated testimonials. Ask them to quantify what changed after they paid—was it a five percent improvement or a fifty percent one? Vague praise doesn't protect your deposit. Request specific before-and-after metrics tied to the same scenario you are facing.
Give yourself a cooling-off window before approving the transfer. Genuine providers rarely pressure you to pay immediately because their results can withstand scrutiny. If the other side becomes impatient or dismissive when you ask for more detail, that reaction itself is information about whether the performance claims deserve your trust.
From Port to Production Floor: Pain Points in Delivery and Commissioning
The moment a shipment clears customs, the clock starts ticking on a chain of assumptions that rarely survives contact with the real world. Port congestion, unexpected inspections, or a missing packing list can stall a critical component for days, while the project schedule quietly slips. What makes it worse is that these delays often surface only when someone physically checks a container or tries to book a truck, turning a supposedly linear handoff into a series of reactive phone calls and temporary fixes.
Once equipment finally arrives at the facility, commissioning brings its own set of unglamorous pain points. Drawings that don't match the installed base, software versions that drifted during transit, or a commissioning engineer who discovers that a critical cable was left behind at the port staging area. Each mismatch forces crews to improvise, which can void warranties or create safety trade-offs that nobody wants to document. The result is a production floor that limps along in manual mode far longer than planned, while the project burns through contingency budget and patience.
Perhaps the most draining part is the administrative fog that surrounds every delay. Delivery receipts get lost between freight forwarders and site managers, commissioning checklists are updated on paper after the fact, and lessons learned rarely make it back to the logistics team for the next shipment. Without a shared, real-time view of what left the port, what arrived, and what actually works on the floor, companies end up paying twice: once for the hardware, and again in overtime, expedited parts, and production downtime.
FAQ
Look past the glossy brochures and ask for a detailed drawing of the blast wheel assembly and the abrasive recovery system. A manufacturer with real engineering depth will be able to explain how the wheel blades are mounted, what materials are used for the liners, and how the separator adjusts for different abrasive sizes. If they only push standard models without asking about your part dimensions, surface requirements, or production volume, that is a red flag. Also check whether they do in-house stress analysis on the chamber and conveyor rollers—many small workshops simply copy designs without understanding cyclic loading.
Request a breakdown of the abrasive flow rate and the capacity of the bucket elevator and air wash separator. Ideally, the system should recycle at least 3 to 5 times the blast wheel's throwing volume per hour. For dust collection, ask about the filter media type and whether the unit includes a pulse-jet cleaning system. Cheap cartridge filters clog quickly with metallic dust, forcing frequent shutdowns. If possible, ask for a reference customer running similar parts for at least two shifts a day, then call that customer directly.
One recurring issue is sizing the roller conveyor for the wrong maximum part weight. Buyers often focus on blast wheel power but forget that the rollers and drive chain must support the full load at speed for hours. Another mismatch is the abrasive type: some Chinese manufacturers default to steel shot when the application really needs a mix of shot and grit to remove mill scale without peening the surface. Also watch the working height—operators may need to load and unload manually, so a non-adjustable height that looks fine on paper can cause ergonomic bottlenecks.
Often the difference is in liner material and thickness. A low quote may use manganese steel plate that is 8 mm thick instead of 12 mm or use ordinary steel for the blast wheel housing, which wears through in months. Another common cost cut is the blast wheel itself—some suppliers use cast iron blades with a short life instead of high-chrome alloy blades. The control system may also be a basic relay panel rather than a PLC with inverter control on the conveyor speed. Ask for a line-item breakdown of chamber plate thickness, abrasive valve type, and electrical components; if they cannot provide it, the low price is likely hiding those gaps.
Do not rely on promises in the proposal. Ask for the names and contact details of at least two existing clients in your region or a similar time zone, and find out how quickly a technician can be dispatched if a major fault occurs. Also check whether they keep common wear parts—blades, liners, seals, filter bags—in stock, and whether they will ship them by air or only by sea. A strong sign is a manufacturer that offers remote diagnostics via a VPN connection to the PLC; that suggests they are serious about supporting equipment after it leaves China.
Roller load capacity determines whether the conveyor will sag or stall under heavy parts, which changes the blast angle and leaves shadowed areas. Blast wheel placement is equally critical: a single wheel mounted only on top will not clean the underside of complex parts, while poorly angled side wheels can erode conveyor rollers faster than the parts. A good design uses overlapping blast patterns from multiple wheels, with the blast direction slightly offset from vertical so that abrasive bounces away from the roller bearings. Ask for a simulation or at least a diagram showing the blast shadow zones on your specific part profile.
Yes. One hidden cost is the abrasive media itself: the machine may be cheap, but if the separator is inefficient, you will consume 30 to 50 percent more steel shot per ton of processed parts. Another pitfall is customs and inland transportation—some Chinese manufacturers quote FOB only, leaving you to handle port charges, duties, and final positioning. Lead times also slip when the manufacturer relies on outsourced casting and machining; ask if they pour their own liners and balance their own blast wheels in-house. Without that, a promised 60-day delivery can quietly become 120 days.
Conclusion
A spec sheet rarely reveals how a roller conveyor shot blasting machine will behave with your actual parts. Suppliers can list impressive dimensions and cycle times while the real bottlenecks only surface when your castings, fabrications, or profiles jam at the transfer points or come out with uneven coverage. The frame thickness, turbine quality, and dust collection system are where many manufacturers quietly cut costs, and that directly affects longevity and operator safety. Matching the blast media to your surface profile requirements and adjusting conveyor speed for part geometry is not a one-size-fits-all setting; getting it wrong leads to rework, media waste, or mechanical jams that stop production.
After the sale, the difference between a smooth production ramp-up and months of downtime often comes down to spare parts availability and how honestly the supplier handles performance verification. Some Chinese manufacturers offer aggressive pricing but minimal local service, so you need to test documented blast coverage and cleaning rates before any deposit moves. Delivery and commissioning bring their own friction: port delays, incomplete installation manuals, or technicians who cannot troubleshoot under real shop conditions. Buyers who visit the factory, speak with existing users, and demand a detailed commissioning checklist are far more likely to get a machine that actually performs as promised on the production floor.
Contact Us
Contact Person: Bruce
Email: [email protected]
Tel/WhatsApp: +86 15166629468
Website: https://www.povalchina.com/