Custom M12 Connector Design Tips for Reliable Industrial Connections
2026-11-16
Industrial connectors rarely get the spotlight until a single loose pin halts an entire production line. M12 connectors are the quiet workhorses of factory automation, but off-the-shelf designs often miss the mark when vibration, washdowns, or tight panel spaces come into play. Custom M12 connector design isn't just about changing pin counts—it's about matching materials, keying, shielding, and cable strain relief to the real conditions on your floor. At REUNION, we've seen how small design choices can prevent costly downtime or create it. This guide walks through practical tips for specifying custom M12 connectors that hold up where standard parts fail, so your next connection won't become the weakest link in the system.
Start with Field Conditions Before Choosing Contacts
Many teams rush into picking contacts first, only to realize later that the audience doesn't fit the campaign's logic. That approach often leads to messy segmentation and wasted sends. Instead, begin by defining the field conditions that matter for your message. Think about behavioral triggers, lifecycle stage, or purchase history before you ever look at a list of names. When the conditions come first, the contact selection becomes a natural result rather than a forced match.
This shift also makes your workflows easier to explain and adjust. Rather than asking "who should get this?" and guessing, you ask "what has this person done, or not done, that makes them relevant right now?" You can then layer simple rules — opened a specific email, visited a pricing page, or hasn't engaged in 60 days — and let those conditions surface the right people. The list becomes evidence, not intuition.
Over time, starting with field conditions keeps your database cleaner and your campaigns more consistent. If a new contact meets the same conditions, they automatically enter the same flow. If someone no longer fits, they drop out without manual cleanup. That kind of clarity is hard to achieve when you pick contacts first and try to justify the audience afterward.
Seal the Interface, Not Just the Shell
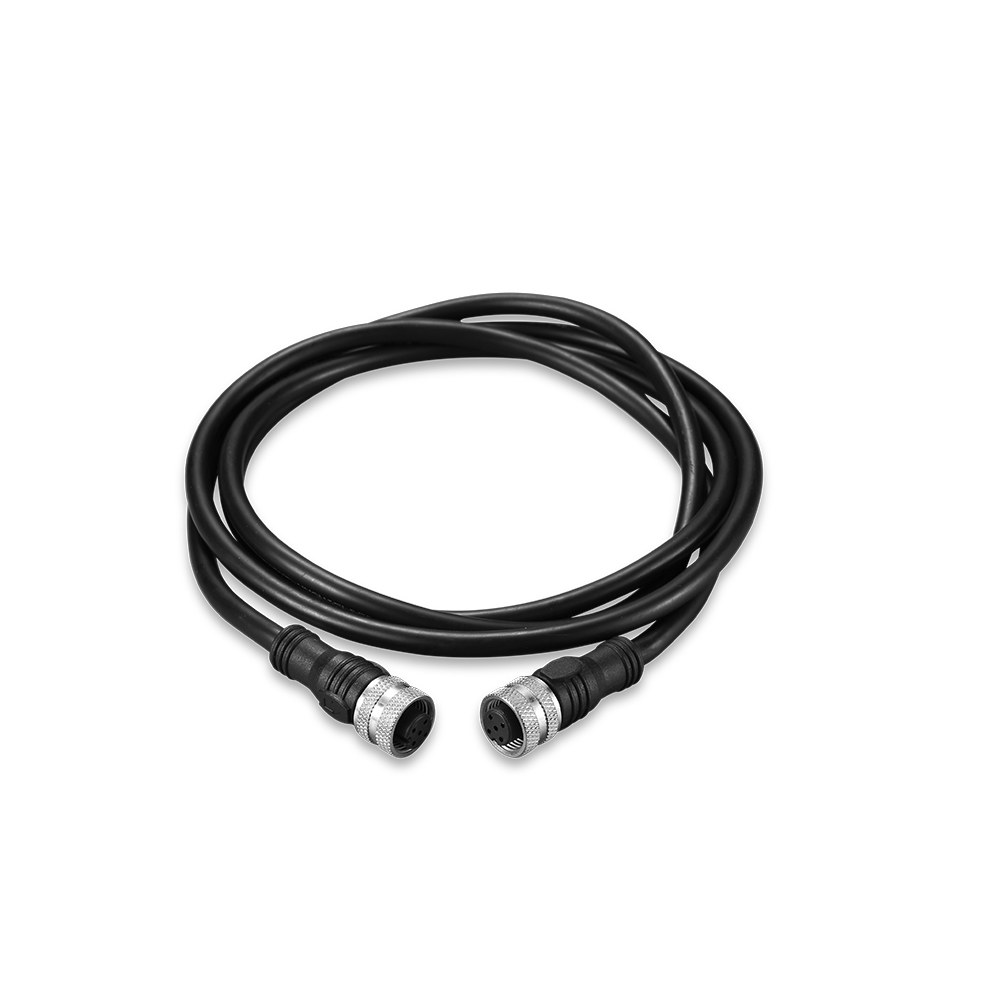
A well-gasketed housing means little if every connector, button, and vent remains an open invitation. The real work happens at the interface, where a cable passes through a wall or a display sits behind an adhesive bead. Those transitions flex with temperature shifts, vibration, and routine handling, so the seal needs to follow that movement rather than fight it.
Start by treating each opening as its own environmental boundary. A formed-in-place gasket around a port can handle slight misalignment, while a rigid O-ring groove may hold only until the first thermal cycle. For cable entry points, consider strain relief that keeps the outer jacket stable so the seal is not peeled back by ordinary pulling. The goal is continuity across the entire surface, not just confidence in the enclosure's main seams.
Testing should deliberately stress the weak points. Dunk the assembly with cables attached, flex the harness, and cycle the temperature while the device is powered. Failures will almost always show up where materials meet and movement concentrates. Fixing those areas often requires less material and more attention to geometry, choosing a softer durometer or adding a drip edge before moisture can reach a vulnerable connector.
Pin Count Is Only the Beginning of Signal Planning
Pin count becomes less meaningful the moment you start mapping return currents. A connector with 240 positions can still force a bad day if two high-speed buses share one return pin on the wrong side.
The initial floorplanning should be driven by current loops and edge rates, not by the neat order of the schematic symbol. Grouping a clock, its return, and its terminator within the same row often saves more signal margin than tuning trace impedance later.
Power and ground discipline shows up before routing does. Assigning pins with nearby planes and avoiding isolated grounds near fast edges keeps the board quieter than adding extra capacitors after the fact. That early attention to pin arrangement is what separates a robust layout from one that merely has enough contacts.
Match Overmolding Materials to Real Thermal Loads
Most overmolding failures trace back to a simple habit: comparing a resin's datasheet value against a single temperature number. Real thermal loads rarely behave that way. A housing near an exhaust manifold, a power tool grip left in a hot truck, or a medical device going through repeated autoclave cycles all impose different rates of heating, peak dwell times, and cooling gradients. Those conditions affect how the overmold holds its shape, keeps adhesion, and resists localized softening far more than a generic HDT or Vicat rating.
Instead of relying on steady-state ratings, instrument the actual part during its worst normal use. Attach thermocouples at the bond line and near thin edges where heat concentrates. Capture the shape of the thermal curve, not just the maximum. A material that survives 150°C for ten minutes may creep badly if it sits at 120°C for six hours under clamp load. Thermoplastic elastomers and TPUs especially shift behavior under sustained heat, losing compression set or becoming brittle after repeated cycling, even when their short-term numbers look acceptable.
Then match those curves against candidate materials using dynamic mechanical analysis or long-term heat aging data. Pay attention to differential expansion between the substrate and the overmold; mismatched CTE can peel the interface long before either material softens. Choose a grade with enough headroom for peak events, but do not chase a higher rating than the measured load demands. Overspecifying often adds cost and processing trouble without improving field life.
Design the Locking Feel for Gloved Hands
Gloved fingers lose the fine joint feedback that bare hands rely on. A lock that feels crisp against skin can turn vague through a few millimeters of insulated fabric, so the cue has to shift away from the fingertip and into the palm, thumb web, and the base of the index finger. Broad, slightly dished release surfaces tend to matter more than a sharp detent that only reads well without gloves.
Texture also behaves differently under a glove. Knurling that grips skin can skim across nylon or leather, especially when wet. The pattern needs deeper spacing and softer edges, enough to catch the glove material without snagging seams. A generous ramp or shelf gives the thumb a clear place to push, removing the need to see the mechanism while working.
The final lockup should register in the hand, not just the ear. A low, solid thunk through the handle and a visible shift in the lock bar reduce doubt when wind, hoods, or machinery muffle sound. Once a gloved user can confirm the state by feel alone, the design stops fighting the hand and starts working with it.
Prototype with the Cable Exit Angles You Actually Use
Cable routing rarely matches the neat right-angle drawings from early concepts. Building a prototype with the exit angles you will actually use forces those mismatches to surface before the design hardens. A connector that leaves the housing at 90 degrees on paper may need a shallow 30-degree departure to clear a chassis rail or avoid a nearby fan. If the prototype only ever tests the idealized angle, strain relief, bend radius, and service loop behavior stay guesses until the first field unit.
The value shows up in assembly and maintenance rather than just electrical performance. Different exit angles change how much force is needed to seat the cable, where the jacket scrubs against edges, and how naturally the cable lays in its retention clips. Using the real angle in a prototype also reveals whether the chosen overmold or boot can hold that shape without kinking. Small changes here often prevent late-stage redesigns that are far more expensive than an extra test fixture.
It helps to create a short list of the actual routing directions from the physical layout: straight back, downward at 45 degrees, side exit, or a compound bend around a nearby bracket. Test those exact orientations rather than whatever off-the-shelf sample happens to be available. The prototype then becomes a reliable stand-in for the installed environment, giving you data about longevity and fit that a generic angle cannot provide.
FAQ
Start with cable retention and strain relief at the rear of the connector. If the cable can flex, rotate, or vibrate near the termination point, look for an overmolded rear boot or a threaded strain-relief clamp rather than a plain gland. Also confirm the internal solder or crimp connections are potted or otherwise supported so the wires don't work loose over time.
Treat the connector as part of the transmission line. Match the impedance across the cable, termination, and connector body. Use shielded variants with a 360-degree clamp to the housing, not just a drain wire. Keep the twisted pairs as close to the terminals as possible. If you're pushing higher data rates, ask the supplier about crosstalk and return loss plots for the full assembly, not just the raw connector.
Mechanical fit is not the same as electrical approval. Mixing power and signal in an A-coded shell can cause crosstalk, heat buildup, and safety issues if a fault puts supply voltage on a signal line. Better to split functions across separate codings or use a multi-coded housing with clear separation and appropriate current ratings per pin.
Look beyond the IP67 rating on the datasheet. The sealing surfaces need to survive repeated mating cycles, temperature swings, and chemical exposure. Ask about the O-ring material, whether the housing is stainless or nickel-plated brass, and if the connector stays sealed when mated and unmated. For washdown, consider a vented cap or a design that avoids water pooling around the coupling nut.
That depends on the contact plating and the wiping action. Gold over nickel gives better cycle life and low contact resistance than tin, but the thickness matters. Ask the vendor for cycle-test data at your expected current and environment, not just a generic number. Also evaluate the locking mechanism. A bayonet or quick-lock variant may reduce wear better than a standard threaded nut if operators change tools frequently.
They define the connector body but forget the full assembly environment. The cable jacket material, bend radius, panel cutout tolerance, and outgassing or UV requirements can invalidate a connector choice faster than pin count. Give the supplier a real application sketch and operating envelope, not just an electrical schematic.
Sometimes, but it's not free. The coding defines the keyway and prevents mismating, not the number of pins. You may find 4-, 5-, and 8-pin versions under the same coding, but higher density means smaller contacts, lower current capacity, and more sensitive termination. Check the derating curve before assuming a pin count swap is safe.
Not always. Inside a cabinet, surrounding noise may be low enough that an unshielded cable works, but you still need to consider ground loops and common-mode noise from drives. If you omit shielding, keep the run short, route away from power leads, and make sure the device at both ends has a proper ground reference. Otherwise, a shielded connector becomes cheap insurance.
Conclusion
Reliable M12 connector designs start long before the drawings are finalized. Field conditions often dictate contact selection more than datasheets do; vibration, washdown exposure, and temperature swings can make a seemingly standard pin set fail early if those stresses are not mapped first. Sealing deserves the same attention at the mating face as at the rear housing, since moisture tends to travel along the contact interface rather than only through the shell. Pin count is rarely the full signal story either. Mixed current levels, shielding needs, and separation between noisy and sensitive lines can reshape a layout even when the total number of positions stays fixed.
Material choices need to follow the actual thermal load, not a generic overmolding spec. A cable that runs near a motor or under direct sunlight will stress a jacket differently than one in a climate-controlled cabinet, and the overmold should reflect that. The locking mechanism also has to be legible through gloves: a positive click or a firm thread stop gives an operator confidence without requiring fine finger work. Prototype with the exit angles and bend radii that appear on the real installation as well, because a connector that works on a bench can fail quickly when the cable is pulled sideways against a machine frame.
Contact Us
Contact Person: Hayley Liang
Email: [email protected]
Tel/WhatsApp: +86 13480625451
Website: https://www.reunion-china.com/