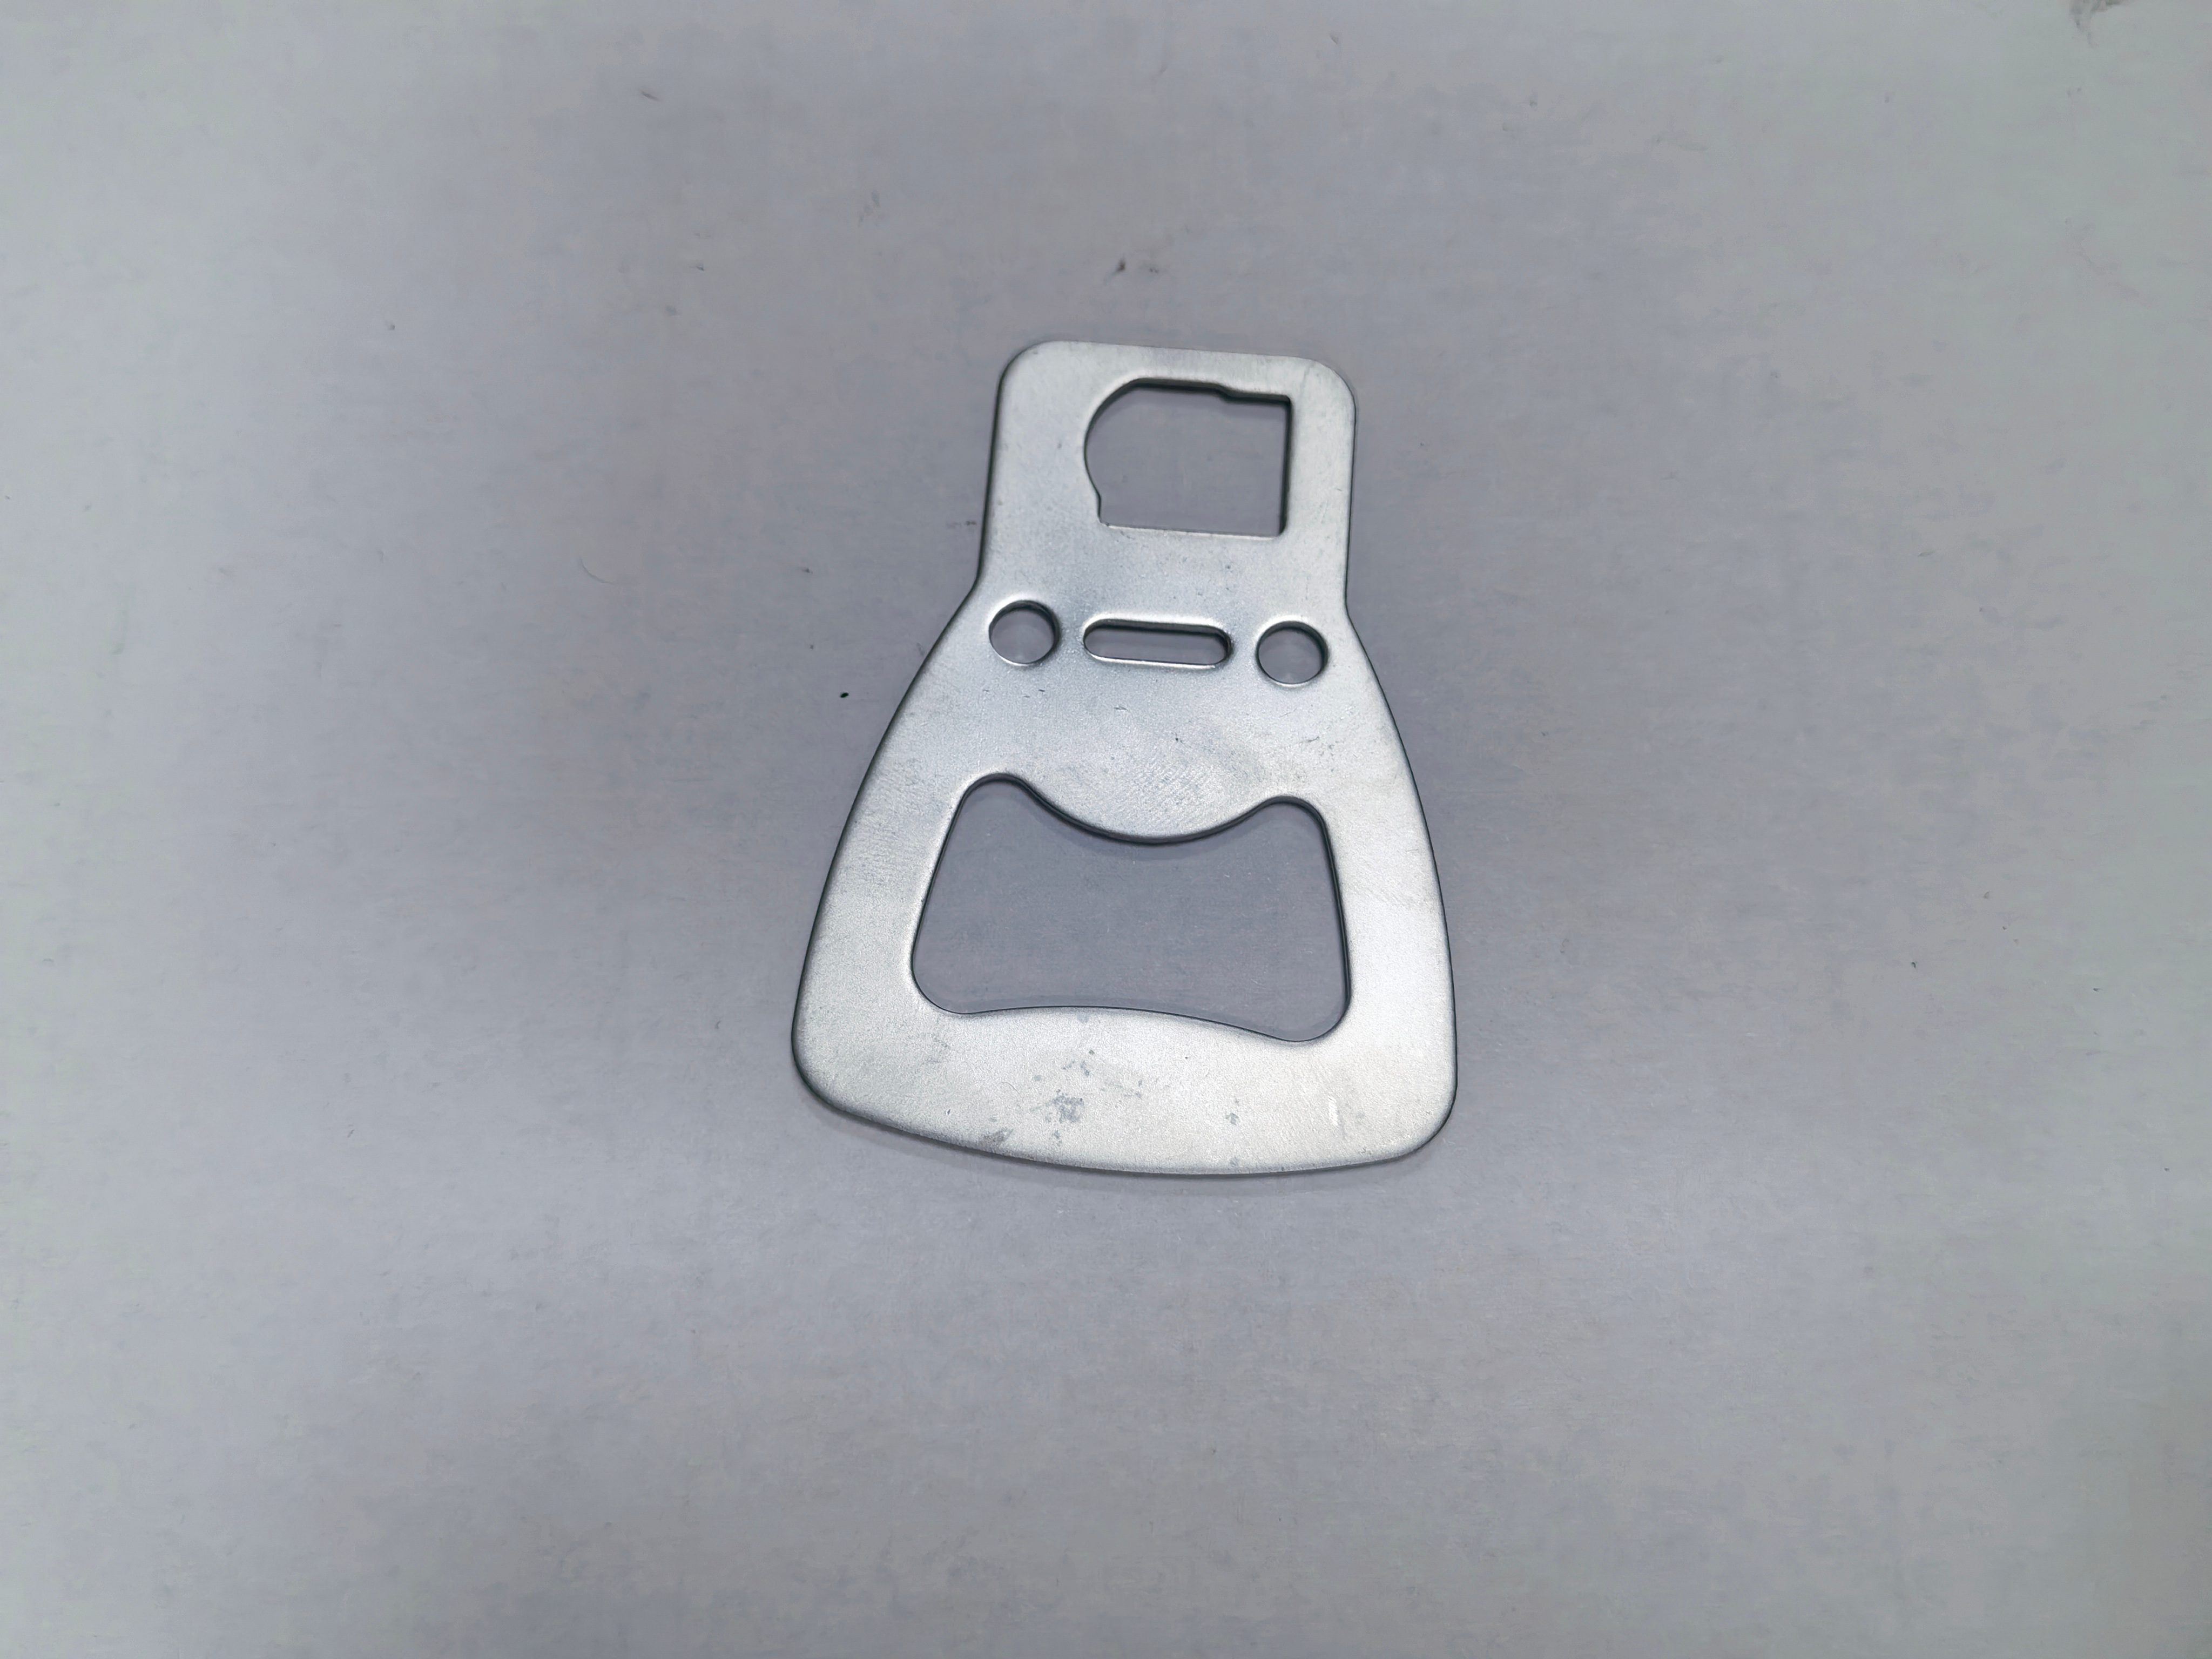
ODM Stamping Parts for Precision Metal Component Manufacturing
2026-11-16
Tooling tolerances rarely survive first contact with a high-speed press. Corners stretch, burrs appear, and a part that measured perfectly at the prototype bench suddenly refuses to fit downstream. For OEMs sourcing ODM stamping parts in precision metal component manufacturing, that drift is expensive. BOYIKUN approaches this differently — building tooling, material specs, and inline checks around the actual stamping process rather than around a CAD file. Here’s what that means for your next component run.
Where Precision Stamping Stops Being a Guess
Precision stamping earns its name only when the numbers on the drawing match the parts coming off the line without a trail of trial-and-error behind them. Guesswork shows up as burr height drifting through a shift, hole positions that wander after tool maintenance, or material springback that nobody accounted for until inspection. Removing that uncertainty starts with treating die setup and press parameters as variables to be measured rather than habits to be repeated.
That shift happens when in-process measurements feed back into tool compensation, and when material lots are checked before they reach the die, not after scrap has already piled up. A stamping process becomes repeatable when operators can read tonnage profiles, strip position, and part geometry at the same cadence as production. Once those signals are visible, adjustments are made from evidence instead of instinct, and the line stops depending on whoever happens to be running it that day.
The difference shows up over thousands of cycles. Tools wear, lubricant thins, coil tension shifts, and the process either holds its tolerances or quietly drifts. A mature precision stamping operation tracks that drift before it reaches the part, using historical run data to set control limits that mean something on the floor. At that point, quality is not a sorting step at the end; it is designed into the way the press is set, monitored, and adjusted.
Tooling Decisions That Make or Break Repeatability
Most teams claim they want repeatable builds, but the toolchain they choose quietly decides whether that actually happens. A package manager that resolves floating versions, a Dockerfile that pulls from a mutable tag, or a CI cache keyed only by branch name can all turn the same commit into different artifacts. The first place to look is not the team's discipline—it's the defaults baked into their tools. Lockfiles, digest-pinned base images, and dependency mirrors are not extras; they are the difference between a build that can be recreated in six months and one that only worked on someone's laptop.
Some tools make reproducibility the path of least resistance, while others make it a constant fight. With pip you have to remember to freeze requirements; with uv or Poetry the lockfile is central. With Docker you can pin by digest, but many registries and tutorials encourage latest. The useful question is not whether a tool can be forced to be repeatable—almost anything can with enough scripting—but what it does when nobody is paying attention. If the default allows versions to drift or timestamps to leak into artifacts, that default will eventually bite.
Tooling decisions also extend to the toolchain itself. Two developers on the same commit can get different formatted output, test results, or compiled binaries simply because their compilers, linters, and runtime versions differ. Version managers like mise or asdf, pinned base images, or fully locked dev containers remove that noise. When every command runs through an explicitly versioned toolchain, the phrase 'works on my machine' loses its meaning—and that is exactly the point.
Material Specs We Won't Compromise On
We tried a lighter canvas once. It felt great on day one, broke in fast, and then turned sloppy around the seams after a single season. The 20-ounce cotton we use now is not forgiving. It arrives stiff, takes weeks to soften, and rewards patience with a structure that actually outlasts the zipper.
Hardware gets the same scrutiny. Cast zinc pulls were cheaper and looked identical in photos. They snapped under load. We moved to solid brass YKK sliders and #10 teeth, then added a locking mechanism because an overstuffed bag should not unzip itself on a bike rack.
Thread and edge finishing are the quiet places where most products cut corners. We use bonded nylon at every stress point, double-stitched with a walking foot. Leather edges are burnished by hand instead of being hidden under paint. It takes longer and costs more, but you notice the difference after about a year of rough daily use.
Small Features, Tight Tolerances, Zero Excuses
The difference between a part that fits and a part that almost fits usually comes down to details nobody notices until they fail. Small features are where that truth lives. A tiny chamfer, a recessed shoulder, a radius tucked behind a thread — these aren't decorative flourishes. They control how loads travel, how seals seat, and how long an assembly holds up in the field. Skipping them or letting them drift is how good designs turn into warranty claims.
Tight tolerances don't mean chasing zeros on a drawing for the sake of it. They mean understanding which dimensions actually carry the function, then controlling those with real process discipline. The goal isn't a perfect inspection report every time; it's a part that behaves the same way at the edge of the tolerance band as it does in the middle. That demands stable fixturing, sharp tooling, and the willingness to stop a machine before it quietly produces a day's worth of scrap.
Zero excuses is the part that can't be machined or measured. It shows up in how problems get reported, how revisions are handled, and whether a supplier treats a near-miss as a warning or an inconvenience. When small features are respected and tight tolerances are backed by honest process control, the excuses mostly disappear — because the work already answered the hard questions before the parts left the floor.
Why Your Drawing Isn't the Whole Story
A sketch can feel like a finished thought, especially when the lines finally sit right. But what you put on paper is only the visible edge of a much larger process. Every mark carries hours of looking, doubting, erasing, and second-guessing that never make it into the frame. The drawing becomes a record of decisions, not just a picture of a thing.
People often judge a work by whether it resembles something recognizable, yet the real content lives in the gaps between intention and accident. A smudged thumbprint, a line gone slightly too far, a shadow you didn't plan but decided to keep — these are pieces of your attention working in real time. They tell a story about how you see, not just what you saw.
So the next time a drawing feels incomplete or less than impressive, remember that its value isn't limited to the final image. What you learned while making it, the patience you practiced, the choices you rejected, and the moment you knew to stop — those are invisible layers no viewer can fully recover. The drawing is a door, not the whole room.
Scaling from Pilot Runs to Full Production Without Losing the Edge
Pilot runs tend to reward improvisation. Small teams can tweak fixtures, adjust cycle times, and talk through problems in minutes. Full production, however, pulls those informal habits apart unless they are captured while the pilot is still running. The most practical move is to document the adjustments that actually worked, not the process someone originally planned.
Scaling usually fails when managers treat volume as a simple multiplier. A tenfold increase in orders does not mean the same process with more hours; it changes material flow, quality checks, and how fast decisions need to travel. Keeping the edge means protecting the short feedback loops that made the pilot responsive, even as more people join and shifts lengthen.
One way to do that is to lock down critical tolerances early and leave room for operators to refine non-critical steps. Teams that keep daily stand-ups tied to real pilot data can spot drift before it becomes a permanent flaw. The goal is not to reproduce the pilot exactly; it is to carry forward the same willingness to notice small problems and fix them before they grow.
FAQ
It's more than running the press. The supplier should be able to take a rough concept or a finished drawing, refine the design for manufacturability, select the alloy, build the tooling, and validate the process so your incoming parts are stable from the first batch.
Look at the quantity, the number of forming steps, and how tight the feature-to-feature position tolerances are. If a part needs piercing, bending, and cutting at high volume, progressive tooling keeps everything indexed in one strip. Lower volumes or very simple shapes often don't justify that upfront tooling cost.
Many precision stamping programs hold ±0.05 mm on standard features without much trouble. Tighter than that is possible on select dimensions, but only when the material, tool design, and secondary operations are planned together. Springback and strip movement tend to set the real limit.
Stainless steels, phosphor bronze, beryllium copper, brass, and cold-rolled carbon steel show up most often. The application usually drives the choice: connectors need conductivity and spring properties, while structural parts may prioritize strength and cost.
In-house stamping only works if you have enough volume across enough part numbers to keep tooling and press time utilized. ODM lets a team tap into existing toolroom expertise and process controls without owning that overhead, which is especially useful when the part mix changes frequently.
Ask for part samples from similar products, not just a machine list. Dig into how they approve first articles, monitor tool wear, and react when a dimension moves out of spec. The best indication is whether they share their limitations clearly rather than claiming every geometry is easy.
Burr direction, bend radius relative to stock thickness, and how the material grain direction affects cracking or springback. These don't always show up in CAD, but they decide whether the tool stays stable and whether the part passes inspection at full speed.
Conclusion
Precision stamping falls apart the moment tolerances become assumptions. In ODM projects, the difference between a stable part and a wandering one usually traces back to tooling choices made before the first hit. We treat die clearance, piloting, and strip layout as engineering constraints, not preferences. A repeatable process starts with material that is not merely "equivalent" to the drawing. Grain direction, temper, thickness tolerance, and edge condition change how metal flows, springs back, and fatigues. When a customer hands us a print that looks straightforward, we ask what happens at the corner radii, at the burr side, and after plating. Those details are where a weak tool drifts and a proper ODM build holds dimension across thousands of cycles.
Small holes, narrow lands, and formed tabs rarely survive production unless the tool is designed around them from the start. Tight tolerances cannot be inspected into a stamping; they have to be built into the strip progression and the die maintenance plan. We also push beyond the drawing because a part that meets the CAD model in isolation can still fail in assembly. Stack-up, springback direction, and secondary operations change the final functional envelope. Scaling from pilot runs to full output is less about running the same tool faster and more about understanding where wear will show up first. By controlling those variables early, ODM stamping parts stay consistent from the first approval sample to the last container without quietly drifting out of spec.
Contact Us
Contact Person: Xianchen Hu
Email: [email protected]
Tel/WhatsApp: 86-13248645200
Website: https://www.hexnb.com/