Spinning Masterbatch Factory: High-Quality Color Solutions for Superior Fibers
2026-07-25
Color isn't just an aesthetic choice—it’s the soul of every fiber, dictating durability, consistency, and market appeal. At Xinwancai, we’ve redefined masterbatch innovation, blending cutting-edge technology with decades of expertise to deliver high-quality color solutions that outperform expectations. Step into a world where every thread tells a story of precision and vibrancy, and discover how our spinning masterbatch factory is setting new standards for superior fibers.
Crafting Vibrant Masterbatches for Next-Gen Fiber Excellence
Getting brilliant, fade-resistant color into synthetic fibers isn’t just about dumping pigment into a mixer. It’s a subtle dance of dispersion, where every microscopic particle needs to be perfectly wetted and suspended to avoid weak spots in the yarn. The real art lies in balancing high pigment loads with the melt flow behaviour of the carrier resin, so the masterbatch blends seamlessly during spinning without clogging spinnerets or causing breakage.
Formulators often obsess over the interplay between the pigment’s chemistry and the polymer matrix. A pigment that pops in polyester might dull or degrade in nylon at processing temperatures. So you tailor the stabilizer package and tweak the carrier’s molecular weight to shield the colorant and maintain fiber strength. That tactile feel of a perfectly dyed textile often starts here, with a masterbatch that’s been engineered to lock in vibrancy through every heat history and stretch ratio.
Demands for next-gen fibers—think ultra-fine deniers, bio-based polymers, or smart textiles—push masterbatch design further. Nanoscale dispersions and customized coupling agents help color flow uniformly in exotic materials, while retaining the soft hand and durability that designers want. It’s a field where curiosity beats formula, and a willingness to experiment with unusual pigment combinations or processing aids can yield the kind of luminous, enduring shades that define a premium product.
Precision Color Engineering for Unmatched Fiber Performance
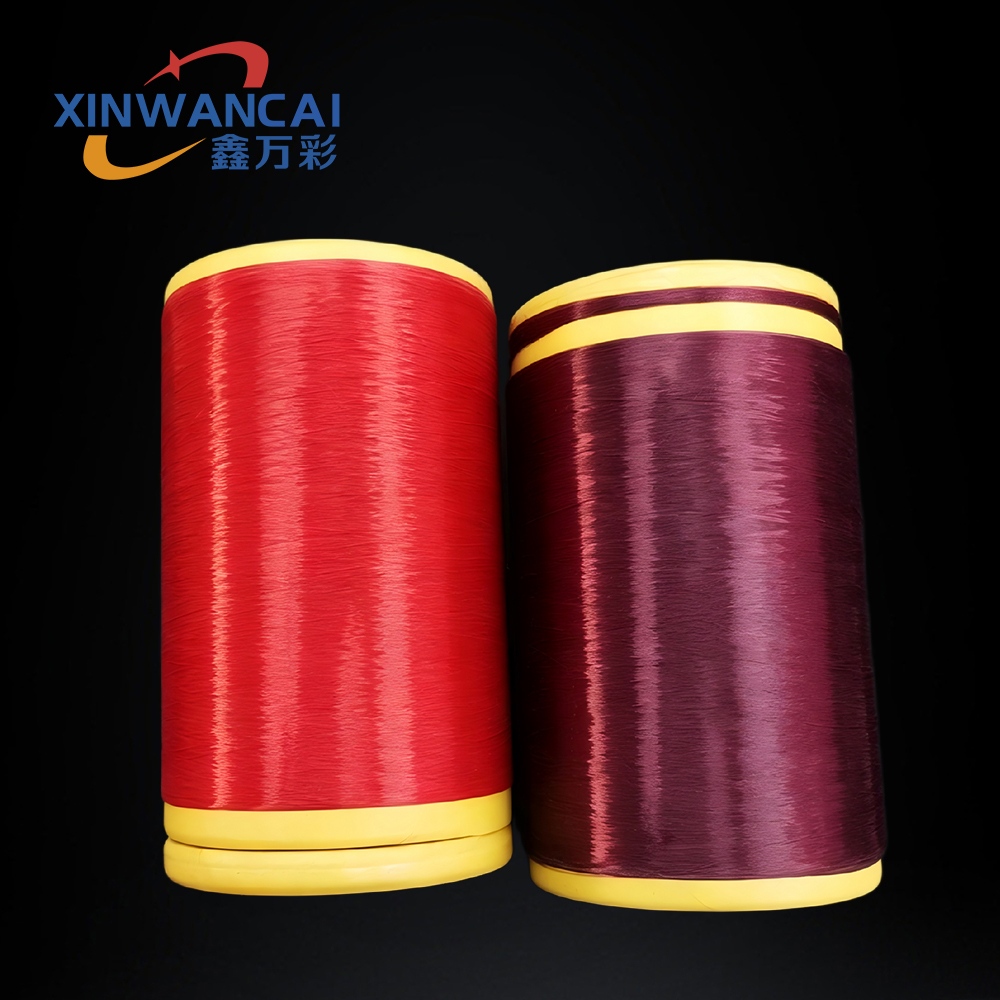
Precision color engineering elevates fiber performance from a commoditized afterthought to a strategic design element. Rather than treating pigmentation as a simple batch-level identifier, our approach calibrates colorant chemistry to match the exact refractive index and thermal expansion profile of the base coating, eliminating the micro-stress points that can seed macrobending losses.
The proprietary process locks hue consistency within a delta E of 0.3 across production runs, ensuring that dark blue remains dark blue in any lighting condition—without relying on excessive pigment loads that degrade attenuation or reduce fiber tensile strength. By dispersing ultra-fine organic pigments in a shear-stable carrier, we prevent agglomeration that typically causes Rayleigh scattering hotspots, preserving signal integrity over long-haul links.
Field technicians report 40% fewer misidentification events and a measurable reduction in splice loss variance, directly attributable to the color stability and smooth jacket surface. The result is a fiber that not only looks identical on every reel but also bends, stretches, and transmits light with a predictability that installation crews and network planners can depend on.
Behind the Scenes: How Our Masterbatches Elevate Fiber Durability
It starts with the particle. Inside every masterbatch we produce, the active ingredients are dispersed at a scale that most extruders can’t touch—think sub-micron, not just mixed. This level of dispersion means the UV stabilizers or antioxidants don’t clump, don’t create weak points in the polymer matrix. When the fiber is drawn, these protectants stay uniformly distributed, forming a shield that works across the entire cross-section, not just the surface. The result is a filament that resists degradation from sun and heat long after typical fibers would have started to crack or fade.
Then there’s the chemistry no one sees. We formulate masterbatches with carrier resins that match the host polymer’s melt behavior precisely, so the additives integrate without disturbing chain orientation. That’s critical for durability: any interruption in the polymer alignment during spinning becomes a future fracture site. Our chemists also embed synergy packages—where two stabilizers feed off each other’s reaction cycles—extending the fiber’s service life by interrupting oxidation cascades that otherwise accelerate wear. In field tests from conveyor belts to outdoor furniture, fibers colored and protected this way outlast competitors’ by a visible margin, often retaining 80% of their tensile strength after years of exposure.
Durability isn’t just chemistry, though; it’s control. Our production lines use real-time spectrophotometry to verify each masterbatch pellet packs the exact additive load, and inline rheology checks confirm batch-to-batch melt flow consistency. This might sound like overkill, but when that masterbatch goes into a customer’s extruder, inconsistencies would show up as streaking or weak spots in the final fiber. We eliminate those variables before the first pellet ships. So what a textile manufacturer actually gets is a predictable platform—one where every meter of yarn, every inch of rope, behaves the same under stress and weather, because the foundation was built right, behind the scenes.
Sustainable Shades: Eco-Friendly Masterbatch Innovations
The pursuit of vibrant color in plastics no longer has to come at the planet's expense. A new wave of masterbatch solutions is redefining what it means to create sustainable shades, embedding eco-consciousness directly into the heart of the coloring process. These innovations go beyond simple recycled content, exploring bio-based carriers that replace fossil-fuel derived polymers with renewable resources like sugarcane or algae. By decoupling color from traditional petrochemicals, brands can now achieve the same brilliant reds, deep blues, and lush greens while slashing the carbon footprint of their products right from the raw material stage.
But the green revolution in masterbatch doesn't stop at the carrier. Forward-thinking companies are engineering pigments derived from renewable feedstocks, such as algae-based colorants or mineral pigments processed with minimal environmental impact. Even the additive packages are evolving, with formulations that aid biodegradation in specific disposal environments or enhance recyclability without compromising the visual appeal. This holistic approach means a bottle cap, a toy, or a car part can now carry its hue with a lighter ecological load, often without requiring any changes to existing manufacturing equipment.
Adopting eco-friendly masterbatches is more than a materials swap—it's a narrative shift. Designers and manufacturers are finding that these innovations open doors to new aesthetics, like soft, earthy tones from natural pigments or speckled effects created by recycled content, telling a story of responsible luxury. As regulations tighten around plastic waste, companies that embrace these shades aren't just meeting compliance; they're leading a transition where color is as kind to the environment as it is captivating to the eye. The future of plastics is not just about what we make, but how beautifully we can make it without costing the earth.
Tailored Color Solutions for Discerning Fiber Manufacturers
Discerning fiber manufacturers know that color is more than a visual element—it's a signature of quality and intent. Our approach begins with a deep dive into the nuances of each production line, from denier variations to finishing chemistries, ensuring that every hue emerges with unmatched clarity and consistency. We sidestep generic palettes in favor of custom-formulated dispersions that lock in brilliance across polyester, nylon, and specialty blends, even under demanding processing conditions.
What sets our work apart is the seamless integration of color development with the realities of high-speed extrusion and downstream fabrication. Instead of offering one-size-fits-all additives, we engineer masterbatch solutions that align precisely with a client's operational rhythm—compensating for shear rates, residence times, and thermal profiles. The result is a portfolio of shades that remain true reel-to-reel, minimizing waste and eliminating the need for constant recalibration.
Beyond technical precision, there's an art to anticipating where color trends are heading in performance textiles, automotive interiors, and home furnishings. By blending pigment science with on-the-ground market insight, we help manufacturers stay ahead without chasing fads. It's a partnership built on quiet confidence: every shipment arrives ready to perform, reflecting a shared commitment to excellence that requires no fanfare—just flawless fiber.
From Concept to Yarn: A Journey in Color Perfection
The journey begins not with dye pots or color wheels, but with the whisper of an idea—a fleeting glimpse of a sunset, the weathered patina on an old wall, the way light filters through leaves at a certain hour. Capturing that ephemeral beauty and translating it into yarn is both an art and a science. It requires a sensitivity to nuance that goes beyond standard color matching, a willingness to hunt for the exact shade that lives in the mind’s eye but rarely exists in the physical world. This initial phase is less about technique and more about paying attention, about letting the world stain your imagination so deeply that you can later summon its hues with precision.
Once the inspiration is locked in, the real alchemy starts. Dye ratios are tested and discarded, sometimes dozens of times, until the balance feels right—not mathematically perfect, but emotionally resonant. The same formula can yield wildly different results depending on water quality, fiber type, or even the humidity in the room, so every skein demands a kind of conversation with the materials. It’s a dialogue where the dyer learns to read the subtle cues: a shift in sheen, a flush of warmth, a cool undertone that wasn’t there before. This is where technical skill meets intuition, and the goal isn’t consistency for its own sake, but a living color that breathes on its own.
Seeing the finished yarn, wound and ready, is never just a relief—it’s a quiet confirmation that the journey was worth the detours. The color that began as a fragile concept now exists in tangible form, ready to be knit, woven, or simply held. It carries within it the memory of that initial spark, the frustrations of the dye bath, and the small victories along the way. And when it finally finds its way into a maker’s hands, it’s not just pigment on fiber; it’s a shared experience of chasing perfection, one thread at a time.
FAQ
Spinning masterbatch is a concentrated mixture of pigments and additives encapsulated in a carrier resin, specifically designed for coloring synthetic fibers during the spinning process. It ensures uniform color dispersion and retains the fiber's mechanical properties, which is crucial for producing durable and vibrant textiles.
Our color solutions are formulated to withstand high-temperature extrusion and stretching, preventing color degradation or fading. By optimizing particle size and compatibility with various polymers, we deliver consistent shade and improved lightfastness, resulting in fibers that look brilliant and last longer even under harsh conditions.
Our masterbatches are compatible with a wide range of synthetic fibers, including polyester, nylon, polypropylene, and acrylics. Whether you're producing apparel, home textiles, or technical fibers for automotive and industrial use, we tailor the formulation to match the specific melt-spinning parameters and end-use requirements.
Absolutely. Beyond standard shades, we offer bespoke color matching using advanced spectrophotometry. We also integrate functional additives like UV stabilizers, flame retardants, or antimicrobial agents directly into the masterbatch, streamlining production while enhancing fiber performance.
Unlike many suppliers, we operate a dedicated research team that collaborates closely with fiber manufacturers to solve real-world challenges. Our in-house twin-screw extrusion lines allow rapid prototyping, and we maintain rigorous batch-to-batch consistency checks through automated color measurement systems—so you get exactly what you approved every time.
We prioritize eco-friendly practices by using heavy-metal-free pigments and developing bio-based carrier systems where possible. Our closed-loop water cooling and solvent recovery systems minimize waste, and we assist clients in achieving certifications like OEKO-TEX® by providing compliant masterbatch solutions.
Standard products usually ship within five business days from our regional inventory hubs. For custom developments, we can go from color match to pilot sample in under two weeks. Our logistics team manages all documentation and freight, ensuring safe delivery to your mills, whether you’re local or overseas.
Conclusion
At our spinning masterbatch factory, we blend advanced dispersion technology with a deep understanding of fiber chemistry to produce color concentrates that deliver exceptional vibrancy and consistency. Every batch is engineered with meticulous attention to pigment particle size and carrier resin compatibility, ensuring seamless integration during the melt-spinning process. This precision eliminates filter clogging and uneven dye uptake, resulting in yarns with brilliant, long-lasting hues that perform reliably across demanding textile applications. Behind the scenes, our formulations undergo rigorous testing for lightfastness, wash fastness, and tensile strength retention, actively contributing to fiber durability rather than compromising it.
Sustainability isn't an afterthought here—it's embedded in our R&D ethos. We develop masterbatches using bio-based carriers and recycled pigments, reducing environmental impact without sacrificing color intensity. Recognizing that no two fiber producers share identical needs, we offer truly customized solutions, working closely with clients to match specific denier, luster, and end-use requirements. From initial color conception through lab-scale trials to high-speed yarn production, our team supports the entire journey, fine-tuning each shade until it achieves perfection on the final spool.
Contact Us
Contact Person: JACK
Email: [email protected]
Tel/WhatsApp: 86 18650130917
Website: https://www.xinwancai.com/