Tissue Converting Equipment Company Tips for Optimizing Your Operations
2026-11-02
Few things frustrate a tissue converting team more than watching a perfectly good machine lose time to small inefficiencies—unplanned stops, excess trim waste, or roll handling hiccups. Over the years, DAXIN has helped operators turn those daily headaches into measurable gains. The secret isn't always a major capital investment; it's often a handful of practical adjustments that compound over weeks. In this post, we'll walk through several field-tested tips for optimizing your tissue converting operations—covering everything from blade maintenance to workflow pacing—so you can boost output without stretching your team or budget. Read on to see which changes are worth making first.
Fine-Tune Blade Pressure for Cleaner Cuts
Most people crank up blade pressure hoping for a faster cut, but that usually leads to burn marks, tear-out, or a wavy edge. Instead, start with just enough downward force to keep the blade engaged without bogging down the motor. On thin stock, reduce pressure until the blade almost floats—this prevents chipping along the cut line. Backing off slightly often produces a noticeably cleaner edge than forcing the tool through the material.
Blade pressure isn't a set-and-forget setting. Different materials react differently: softwoods and plastics need light, consistent pressure, while hardwoods or laminates may require a bit more to avoid vibration. A good habit is to make a test cut on scrap and inspect the edge. If you see burning or deflection marks, ease up. If the cut feels rough or the blade stalls, apply a touch more pressure and keep the feed rate steady.
Regular blade maintenance also plays into pressure control. A dull blade makes you push harder, which creates heat and ragged cuts. Swap or sharpen blades before they get too worn, and you'll find that lighter pressure delivers cleaner results. Pay attention to how the tool sounds, too—when the motor pitch stays even and the blade moves smoothly, you've likely found the sweet spot.
Match Roll Hardness to Converting Speed
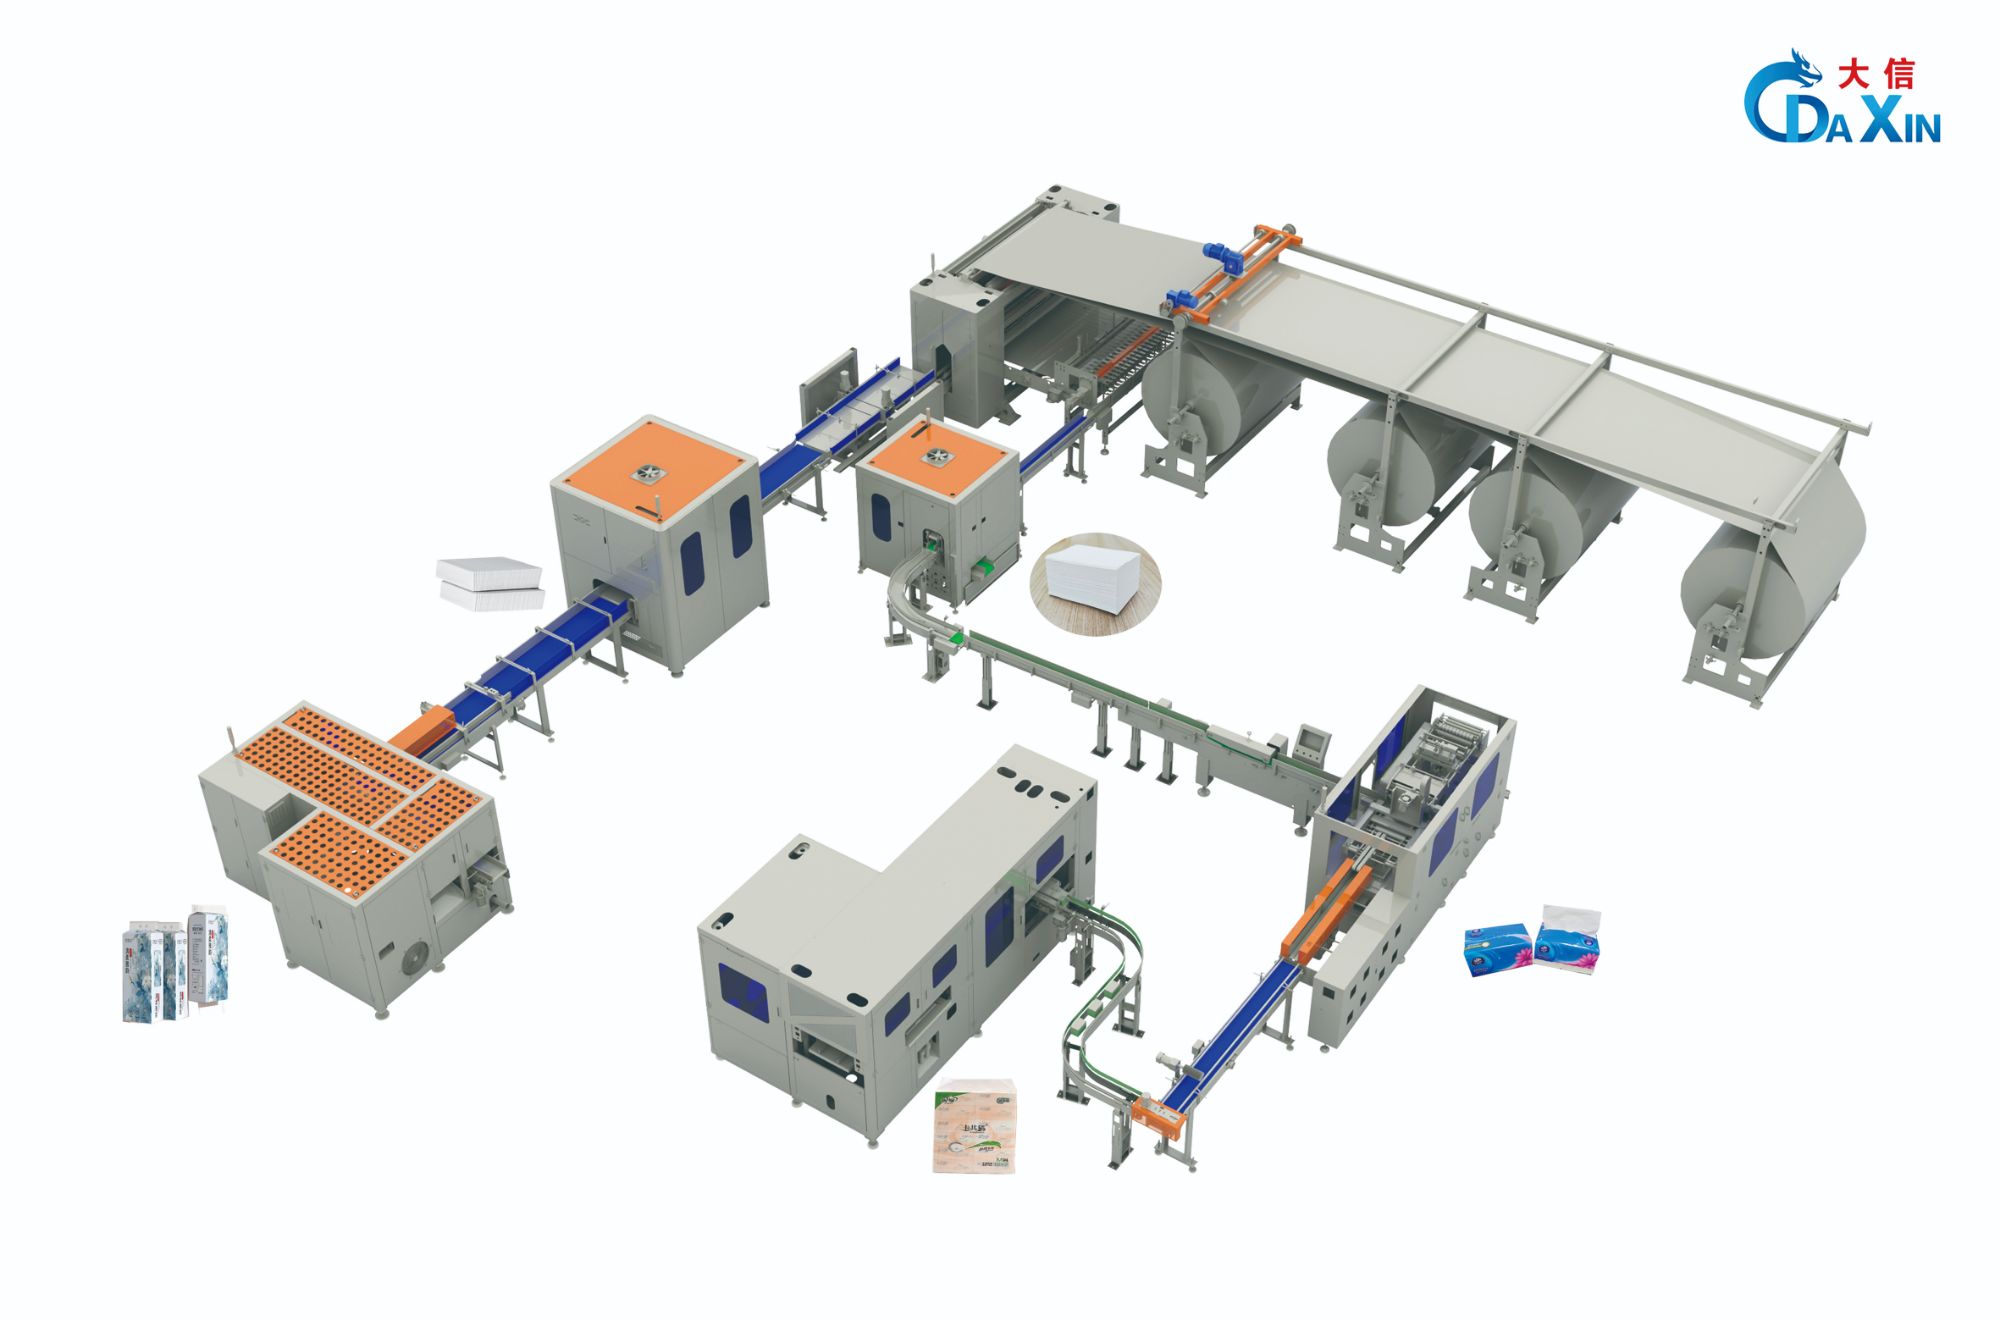
Matching roll hardness to converting speed isn't a one-size-fits-all rule—it's a balancing act that shifts with every job. A roll that feels perfect on a slow laminating line can turn into a wrinkle-prone headache at high speeds, while a overly soft roll may grip the web too aggressively on fast slitters. The key is to treat hardness as a dynamic variable: start with your target speed, then dial in the roll's durometer and crown so the nip pressure stays even from edge to edge. Operators who ignore this often chase defects downstream that could have been solved with a simple hardness tweak at the unwind.
Think of roll hardness as the conversation between the web and the converting equipment. Too hard a roll on a high-speed die-cutter creates chatter and micro-slip, leaving inconsistent cut lengths and ragged edges. Too soft on a slow coating line? The roll deforms and introduces gauge bands that show up as streaks in the final product. The trick is to evaluate the roll's rebound rate—how quickly it recovers after each nip—rather than its static hardness alone. High-speed converters benefit from rolls with a slightly higher rebound, which prevents lingering deformation between rapid contact cycles. This subtle shift in material selection often outperforms dramatic hardness changes.
Practical adjustment starts with a simple test: run the line at 70% of normal speed and feel for vibration. If you notice edge picking or uneven tension, the roll is likely too hard for that speed range. Conversely, if you see center bagging or web wander at full speed, soften the roll by a few points of Shore A. Keep a log of speed versus hardness settings for each substrate—over time, you'll spot patterns that no vendor chart can predict. The goal isn't perfection on the first run, but a repeatable starting point that cuts setup waste and keeps the line moving without constant babysitting.
Schedule Maintenance Around Actual Wear Patterns
Maintenance calendars have a habit of lying. A pump might look fine on paper but carry subtle scoring on its impeller after only a few hundred hours, while an identical unit hums along past its scheduled date without any real concern. Chasing fixed intervals often means pulling parts too early or too late. Instead, track how each asset actually degrades—watch for uneven wear bands on belts, rising vibration signatures, or heat that builds in a bearing long before it fails.
Once you start reading those physical clues, scheduling becomes less about arbitrary dates and more about condition. For instance, if two conveyors move the same material but one shows edge fraying after three weeks, move that belt inspection up while letting the other run longer. This shifts labor and downtime to where they’re truly needed. It also means replacing components before a breakdown, but not so early that you waste remaining service life.
A good approach is to log small observations during routine walkthroughs—squeaks, temperature changes, metal dust, slight misalignment—and let those notes set the next service window. Over time, patterns emerge for each machine, and your maintenance schedule stops being a guess. You end up with fewer emergency calls and a better feel for which equipment needs attention before it becomes obvious to everyone on the floor.
Upgrade Core Handling Before Scaling Output
Too many operations chase higher output while the middle of the process quietly falls apart. The core handling step, whether it is material flow, data processing, or manual assembly, sets the pace for everything downstream. If that step has hidden friction, scaling output only turns a small delay into a daily bottleneck. Early attention here prevents the usual firefighting that follows a rushed expansion.
A practical upgrade starts with watching the core step in real time, not just reading summary reports. Look for repeated waiting, rework loops, or equipment that runs below its rated speed for no clear reason. Often the fix is not a new machine but a simpler change: rearranging the workspace, clearing decision rules, or removing an approval step that adds no value. These adjustments cost little and immediately raise the ceiling for later growth.
Once the core handling is stable, scaling output becomes a matter of adding capacity where it actually helps. Teams that skip this sequence usually end up adding people or machines to compensate for a weak center, which only hides the problem and drives up cost. Building the core first means the expansion has a solid base, and the gains stick instead of fading after the launch month.
Use Operator Feedback to Adjust Tension Settings
Tension adjustments rarely stick when they come only from a manual or a default setting. Operators are the first to notice subtle changes—squealing on startup, belt drift after a load shift, or that slight flutter in the web that never shows up in the maintenance log. Instead of dismissing these as one-off complaints, treat each observation as a live data point. A quick note on the shift board about what the operator felt or heard, along with the current tension reading, creates a trail that reveals patterns faster than any single inspection.
The trick is to make the feedback loop concrete. After an operator flags a tension issue, ask them to mark the exact spot on the speed or load curve where the problem appears. Then make a small adjustment—no more than a quarter turn on the take-up or a 5% change in the controller—and have the same operator run the line for half an hour. If the symptom shifts or disappears, you have a direction. If it stays, you have a different problem, often alignment or wear. This kind of paired test keeps adjustments grounded in what the person at the controls actually experiences, not what the spec sheet predicts.
Don’t let operator feedback end at the adjustment. Record what changed, who reported it, and the before-and-after symptoms in a shared log that operators can access. Over time, that log becomes a troubleshooting shortcut: the night shift operator who hears a new high-pitched whine can scan past entries and see that the last time this happened, a slight reduction in return-side tension solved it for three weeks. That’s the kind of practical memory that prevents repeated call-outs and builds trust between the floor and maintenance.
Reduce Dust Buildup With Targeted Airflow Changes
Most dust problems stem from airflow patterns that unknowingly carry particles toward surfaces where they settle. Instead of simply cleaning more often, look at how air moves through the room. A vent aimed directly at a shelf or electronic equipment will deposit a steady layer of fine dust within days. By redirecting supply registers slightly away from static-prone areas, or adjusting return grille placement to pull air across open spaces rather than over shelves, you can shift the path that dust travels. Small changes in diffuser angle—even ten degrees—can mean the difference between a weekly wipe-down and a monthly one.
In workshops or rooms with high particle generation, creating a slight negative pressure near the source works better than adding more filtration. If a grinding station or printer sits in a corner, a low-volume exhaust fan pulling air away from that spot and toward an outside vent will intercept dust before it spreads. Pair this with a floor-level return near the opposite wall, and you encourage a slow, directional current that sweeps particles down and out rather than letting them swirl upward. No need for heavy equipment—just a deliberate imbalance between supply and return flows can keep airborne dust moving where you want it to go.
Another often-overlooked trick is using air curtains between zones. A narrow strip of downward airflow across a doorway or open pass-through can block dust from migrating from a busy area into a cleaner one, like a vestibule separating a garage from living space. Combined with slight positive pressure in the clean zone, this creates an invisible barrier that costs little to run. The key is to test with a smoke pencil or fine thread to see actual air movement—assumptions about airflow rarely match reality, and a few minutes of observation can reveal exactly where to adjust dampers or fan speeds for a noticeable drop in surface dust.
FAQ
Lubricating the embosser bearings. Many mills focus on blades but forget these, leading to uneven embossing and premature wear. A weekly grease schedule with high-temp food-grade lubricant prevents unscheduled downtime.
Install a dedicated vacuum manifold right after the slitting station. It captures fibers before they settle. Pair it with a regular blowdown using low-pressure compressed air on the unwind stands, but never on running rolls.
Don't rely on hours. Track blade wear by monitoring perforation tensile strength. When it drifts more than 10% from your target, change blades. For most lines running 24/5, that ends up being every 2-3 weeks, but data beats calendars.
Check the core chuck alignment first. A misaligned chuck causes uneven tension during acceleration. Use a dial indicator to keep runout under 0.003 inches. Then set splice ramp speed 15% lower than run speed for the first 500 feet to let adhesive set.
Cross-train but with depth. Start with one primary line until they can diagnose 80% of common faults, then rotate to another line for three months. This builds troubleshooting intuition without diluting expertise. Avoid rotating more often than quarterly.
Switch to a closed-loop glue system with a timer-controlled nozzle. Open trays and manual brushes waste up to 12% of adhesive. Set the nozzle pulse to 0.2 seconds at 60 psi and check the pattern weekly with a cardboard strip.
Graph downtime against speed. If you increase speed by 10% but unscheduled stops rise more than 5%, you're past the sweet spot. The real optimum is where total output per shift peaks, not where the machine can theoretically run.
Conclusion
Getting the most from your tissue converting line starts with the small adjustments that directly affect cut quality and throughput. Instead of relying on factory presets, take time to fine-tune blade pressure—too much force accelerates wear, too little leaves ragged edges, so watch for clean separation on every log. Pair that with roll hardness checks: a roll that is too soft will bounce at higher speeds, while an overly hard roll can crush the sheet and create dust. Matching hardness to your actual converting speed prevents many downstream jams. On the maintenance side, don't just follow a calendar. Track where wear actually shows up—bearings, anvils, knife holders—and let those patterns set your service intervals. That way you replace or adjust what needs it before it causes a line stop, not after.
When you plan to scale output, upgrade core handling early rather than waiting for the line to bottleneck. Adding conveyor capacity, better core chucks, or automated loading may seem like a big investment, but it is far cheaper than unplanned downtime at higher speeds. Tension settings are another area where operators know more than the manual. Gather their feedback after each shift—especially when changing grades or diameters—and adjust unwind and rewind tension in small steps until you see stable web tracking and flat rolls. Dust control often gets ignored until it becomes a quality issue. Instead of general ventilation, look at where dust accumulates and redirect air nozzles or add local extraction exactly there. Targeted airflow changes reduce cleanup time and protect sensitive components, which keeps the whole converting operation running cleaner and longer.
Contact Us
Contact Person: Sam Xie
Email: [email protected]
Tel/WhatsApp: 86-18938538530
Website: https://www.daxin321.com/